Quality Inspection & Assurance
Quality Control for Custom Bench Vises
Stavalk applies project-specific inspection criteria throughout material preparation, casting, forging, CNC machining, heat treatment, assembly, final testing, packaging, and shipment release. Quality Requirements are managed dynamically based on the approved sample, technical specification, artwork proof, Bill of Materials (BOM), and agreed packaging standards for each OEM/ODM order.
Stavalk controls bench vise quality through a 7-stage inspection gate system: incoming material control (IQC), in-process casting and forging inspection, CNC machining verification, heat treatment control, assembly quality control (IPQC), final product testing (FQC), and packing and pre-shipment release (OQC). Every order is inspected against the approved sample, technical specification, artwork proof, BOM, and packaging standards, with clamping force testing, jaw hardness verification, swivel torque checks, dimensional accuracy, accessory confirmation, and batch traceability. Items failing acceptance criteria are placed under controlled hold or quarantine, reworked only under approved instructions, and re-inspected before authorized release.
Specifications verified: 2026-09Our quality system is built for OEM/ODM projects: inspection criteria are defined per order, documented, and followed by production and quality teams from incoming material to packing. This keeps quality expectations aligned between the factory and your brand from the first sample to full container shipments.
Scope
Project-Specific Inspection Criteria
Quality specifications may vary depending on vise construction (e.g., light-duty 2″–5″ jaws, medium-duty 6″–8″, heavy-duty 8″–10″, pipe vises, specialty vises), intended end-use, target market regulations, and customer-approved parameters. Final release authorization is strictly based on the documented inspection criteria agreed upon for the order.
Quality Framework
Our 7-Stage Quality Verification System
A complete QC loop from raw material arrival to shipment release.
- 1
1. Incoming Material Control (IQC)
Raw materials and purchased components are checked against approved specifications and reference samples before entering the production line. HT200/HT250 gray cast iron bodies are verified for chemical composition, tensile strength, and surface porosity. 45# forged steel components are checked for grain structure, hardness, and dimensional tolerances. GCr15/Cr12MoV hardened steel jaw inserts are verified for alloy composition, hardness potential, and surface finish. Hardware, fasteners, and coating materials are matched for quantity, colour, branding, barcode accuracy, and artwork version against the approved BOM.
- 2
2. Casting & Forging Inspection
Sand-cast iron bodies are inspected for mould integrity, pour temperature, riser placement, and gate solidification. Green sand and resin-bonded sand cores are checked for dimensional accuracy and surface finish. Forged steel components are verified for die alignment, forging temperature, flash trimming, and weight consistency against approved drawings.
- 3
3. CNC Machining Verification (IPQC)
Critical machining steps are inspected to catch non-conformities before components move to subsequent workstations. Jaw seat milling is verified for flatness, parallelism, and surface roughness against approved technical drawings. Thread cutting and bore drilling are checked for pitch accuracy, depth, and concentricity. Swivel base machining is verified for rotation smoothness, detent positioning, and mounting hole alignment.
- 4
4. Heat Treatment Control
Heat-treated components undergo mandatory hardness and metallurgical verification before assembly. Jaw inserts (GCr15/Cr12MoV) are quenched and tempered to achieve 58–62 HRC hardness, verified with calibrated hardness testers. Cast iron bodies are stress-relieved to ensure dimensional stability. Forged steel components receive surface hardening where specified. All heat treatment records are logged per batch with temperature curves and hold times.
- 5
5. Assembly Quality Control
Completed vises undergo assembly verification before final testing. Swivel base rotation is checked for smooth operation and detent engagement. Quick-release mechanisms are tested for engagement and disengagement force. Anvil back surfaces are verified for flatness and hardness. Bolt torque, handle operation, and jaw alignment are verified against assembly specifications.
- 6
6. Final Product Testing (FQC)
Completed vises undergo mandatory functional and structural testing before packaging approval. Clamping force is measured at the rated capacity using calibrated force gauges. Jaw parallelism is verified under load with dial indicators. Swivel torque is tested across the full rotation range. Cycle durability testing simulates 10,000+ open-close operations. Salt spray testing (48h+) verifies surface coating integrity on paint, powder coat, or Parkerized finishes.
- 7
7. Packing & Pre-Shipment Release (OQC)
Comprehensive pre-shipment verification ensures zero mismatch in SKU configuration or shipping marks. Kit completeness cross-checks vise, mounting hardware, instruction manual, and customer-specific accessories against the order BOM. Packaging and barcode checks verify carton marks, SKU labels, barcode readability, manual language, and carton structural integrity. Orders are released only after the final packaging audit is signed off by authorized quality personnel.
Inspection Coverage
Key Inspection Control Points
Every checkpoint is executed against documented acceptance criteria agreed per order.
Clamping Force Verification
Completed vises are tested at rated clamping force using calibrated force gauges. Force readings are recorded per unit and compared against the minimum specification. Any vise falling below the rated capacity is rejected and routed through the non-conformance process.
Visual & Dimensional Inspection
Vises are inspected under suitable lighting for surface finish, casting defects, machining marks, coating uniformity, scratches, contamination, and assembly alignment. Key dimensions and jaw positions are verified against approved drawings or specifications.
Accessory & Packaging Verification
The complete product configuration is verified before shipment: vise model, swivel base, mounting hardware, instruction manual, and customer-specific accessories — each matched to the approved sample, drawings, and BOM.
Packing & Shipment Release
Packed units are checked for SKU configuration, accessory completeness, product labels, barcode information, instruction manual version, carton marking, packing quantity, and carton condition. Shipment release is authorized only after all inspection and packing requirements are completed.
Batch Traceability
Project-Level & Batch Traceability System
Every custom bench vise order is managed under a unified project code linking technical specifications, the approved BOM, artwork revisions, material lot numbers, packing references, and inspection records. Production and inspection records are maintained by the applicable project and production batch, and each batch can be linked back to the approved product specification, BOM, artwork, and packing references.
This supports efficient review of product configuration, inspection status, and affected scope if a quality concern is identified — from finished product back to source records using the vise or carton identification.
Traceability Chain
From Project Code to Shipment Release
One chain of controlled references from order confirmation to authorized dispatch.
- 01
Project Code
Unified project reference that links every controlled document to the order.
- 02
Document Revisions
Current spec, BOM, artwork, and packing revision levels — only approved versions are valid for production.
- 03
Batch & Materials
Material and component lots recorded against the production batch.
- 04
Inspection Records
IQC, casting, machining, heat treatment, assembly, final, and packing inspection results per batch.
- 05
Packing & Release
Packing batch, NCR closure status, and authorized shipment release summary.
Anonymized Sample
Traceability Control Record (Demo)
Demonstration values are shown for illustration only — customer names, PO numbers, custom artwork, supplier data, and commercial information are removed to protect confidentiality.
- Manufacturer: Stavalk (Qingdao, China)
- Project Code: DEMO-VISE-2026-01
- SKU Reference: DEMO-BV-600
- Production Batch: BATCH-SEP-01
- Specification / BOM / Artwork Revision: Rev B / Rev C / Rev B
- Clamping Force Test: PASS — retained per batch
- Inspection Status: PASS
- Shipment Status: RELEASED
Non-Conformance Control
Control of Non-Conforming Products & Quarantine
Products or components that do not meet defined acceptance criteria are clearly identified and placed under controlled hold or quarantine status. They cannot proceed to the next production stage, packing, or shipment until an authorized disposition is completed. Rework is performed under approved instructions and linked to the relevant non-conformance record; reworked items are re-inspected against the applicable project requirements before quality release.
7-Step Control Flow
What Happens When a Non-Conformance Is Found
Identify, control, correct, verify — then release or reject. Non-conforming product never flows back into production or packing unchecked.
- 01
Identify
The non-conformance is recorded against the affected product, SKU, batch, or process stage.
- 02
Label
Affected items are clearly identified with controlled status labels — HOLD, QUARANTINE, or REJECTED.
- 03
Quarantine
Items are segregated in a physically controlled quarantine area or system-controlled to prevent unintended use or shipment.
- 04
Assess Scope
The affected scope is reviewed by batch, process stage, material lot, and document revision.
- 05
Rework / Replace
Correction is permitted only through an approved disposition and controlled work instruction.
- 06
Re-Inspect
Corrected items are re-inspected against the applicable acceptance criteria before release.
- 07
Release or Reject
Only authorized conforming product proceeds to packing or shipment release.
On the Factory Floor
Controlled Testing & Quarantine in Practice
Photos from our workshop in Qingdao show how status control and inspection records are applied on site.
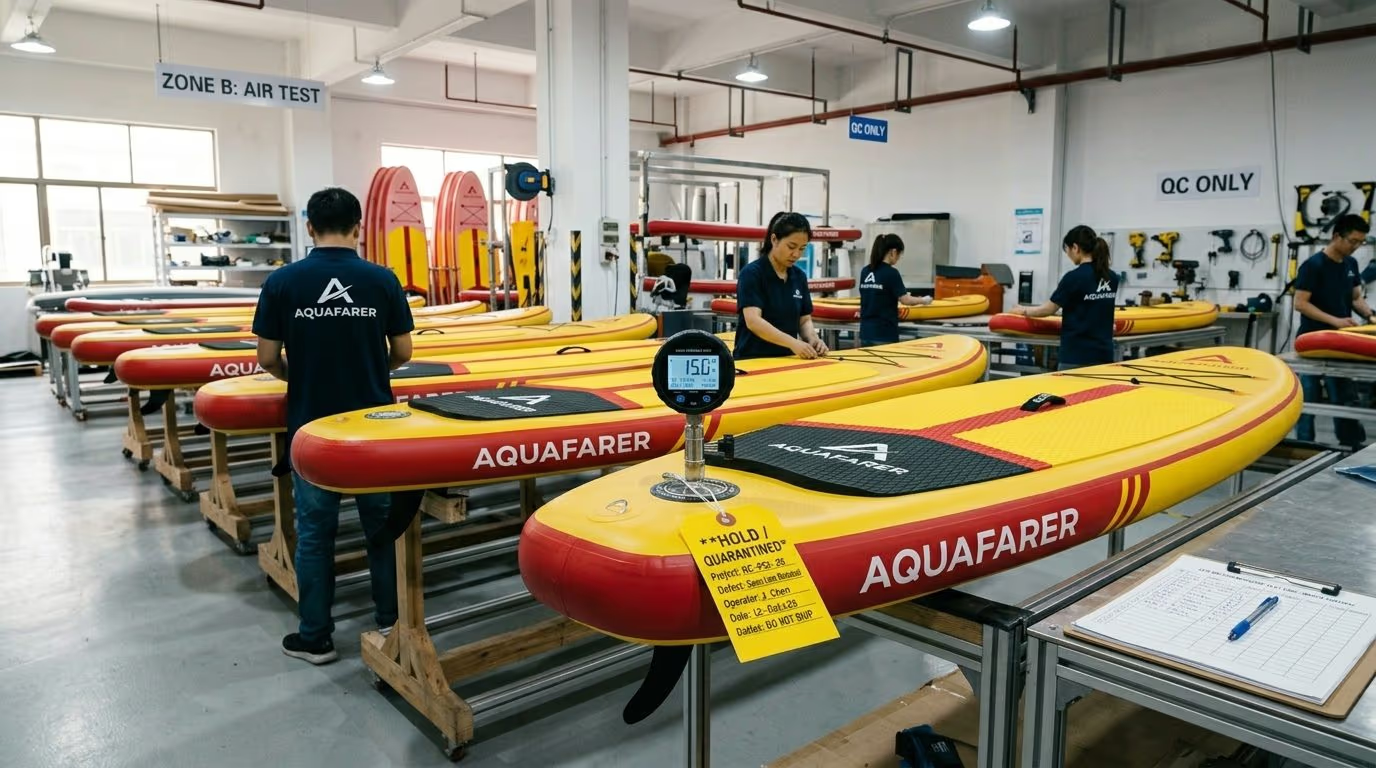
Hold & Quarantine Station
Inspection station with QC checksheets and status labelling. Any item failing acceptance criteria is tagged, logged, and moved to quarantine — it cannot proceed to packing until an authorized disposition and mandatory re-inspection are completed.
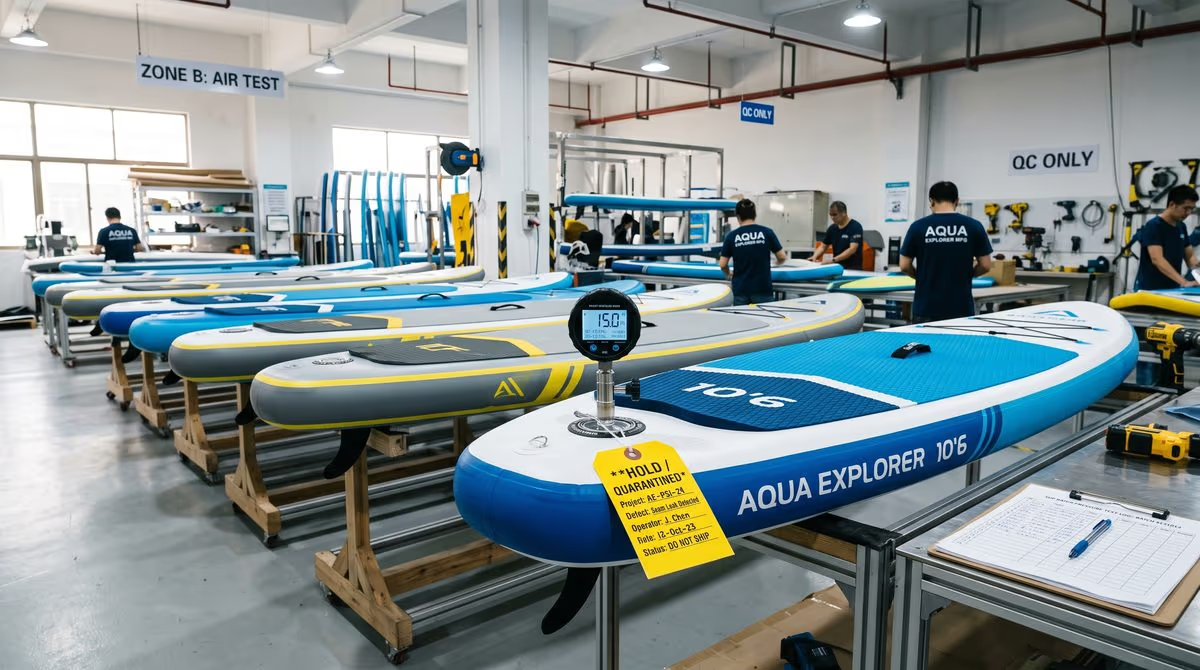
Quarantine Area Demonstration
Demonstration photo from the workshop showing how controlled quarantine segregation works on site: segregated units are kept under status control until an authorized disposition is completed.
Rework Governance
Controlled Non-Conformance & Rework Governance
At Stavalk, rework is defined strictly as restoring a non-conforming unit to full compliance with its original engineering specification — not as a quick fix. Any bench vise identified with a quality non-conformance is placed on controlled hold and linked to a Non-Conformance Report (NCR) before further processing; the defect source is located and recorded using the approved diagnostic method.
Rework may proceed only when the defect is within the approved rework scope and an authorized method is available. The rework instruction identifies the product, batch, defect location, approved material, method, required conditions and re-inspection scope. After the required process, the vise is re-inspected against the same applicable acceptance criteria as a conforming product — rework never reduces the acceptance standard. Failure of re-inspection requires renewed engineering and quality disposition; repeated rework is not permitted without documented approval.
Interactive Flow
Rework Decision Flow — Click Any Node
Follow how a non-conformance is handled from detection to release or scrap. Click a node to expand the control requirements at that step.
A quality non-conformance is identified during inspection — clamping force failure, jaw hardness below spec, surface defect or a related manufacturing defect.
| Defect Category | Typical Area | Rework Eligibility | Required Approval |
|---|---|---|---|
| Class A — Surface Finish | Casting surface, machined surface, coating finish | Standard rework authorized | QC Inspector |
| Class B — Dimensional | Jaw parallelism, bore diameter, thread pitch | Evaluated rework per the approved method card | QC + Engineering |
| Class C — Hardness | Jaw insert hardness below 58 HRC specification | Authorized only when re-heat treatment is feasible | QC + Engineering |
| Class D — Clamping Force | Force output below rated capacity | High risk; strict engineering disposition required | Engineering + QA Head |
| Class E — Swivel Mechanism | Base rotation, detent, quick-release failure | Standard rework not authorized — replacement or root-cause review | QA Head + Customer Concession |
| Class F — Coating | Paint, powder coat, or Parkerized finish defects | Re-coating within approved parameters | Lead QA / Engineering |
| Class G — Structural | Casting crack, forging defect, body deformation | Rework not authorized — replacement, scrap or written customer concession | Quality Manager + Customer Approval |
7-Step Closed-Loop
Controlled Rework Workflow — From Detection to Release or Scrap
Every rework follows the same controlled loop: detect, quarantine, diagnose, authorize, rework, re-inspect, release.
- 01
Detection, Stop-Line & Quarantine
Processing stops immediately on the affected vise. Vise ID, product code, batch, workstation, date and inspector are recorded, a HOLD / QUARANTINE label is attached, and an NCR is opened against the applicable specification revision.
- 02
Systematic Defect Diagnosis
The defect is located with the approved method — visual inspection, calibrated hardness testing, dimensional measurement, or clamping force testing. The suspected location is marked without damaging the product.
- 03
Engineering Disposition & Authorization
QC confirms the defect category and Engineering reviews whether the vise can be restored to its original specification. A rework authorization referencing the NCR records the approved method, materials, conditions and re-inspection scope — or assigns replacement, rejection, scrap or customer concession.
- 04
Controlled Rework Execution
Rework is executed only within the approved defect boundary, using the approved method card, material batch and tooling. Vise dimensions, surface finish, mechanical function and packing requirements are never altered.
- 05
Process Completion & Pre-Check
The reworked vise remains in HOLD status through the rework process defined by the approved instructions, then receives a visual and dimensional pre-check before re-inspection.
- 06
Re-Inspection & Proof Testing
The vise is tested against the project-approved re-inspection criteria and the original failure plus all potentially affected characteristics are re-verified: clamping force, jaw hardness, dimensional accuracy, swivel function, coating integrity, and appearance. Rework never reduces the acceptance standard.
- 07
QA Release or Final Disposition
Quality reviews the completed NCR, rework record and re-inspection result, then authorizes release — or escalates to replacement, rejection, scrap or customer concession. No reworked vise is packed or shipped without authorized quality release.
Quality Safeguards
Anti-Error Rules That Protect Your Brand
Hard controls that prevent uncontrolled repair loops — one documented rework per defect, batch-level alert thresholds, calibrated instrumentation and controlled test conditions.
One Rework Per Defect
A single location may be reworked once under an authorized instruction. If re-inspection still fails, the vise is escalated for replacement, rejection, scrap or customer concession — repeated rework without documented approval is not permitted.
Batch Alert & Line-Stop
When non-conformance in a production batch exceeds the engineering-set threshold, the line is stopped and Engineering investigates the cause — material lot, process conditions and records — before production resumes.
Calibrated Instrumentation
Force gauges, hardness testers, calipers, and torque wrenches used for testing are controlled and calibrated by third-party laboratories within their validity period, with calibration status visible in the inspection area.
Controlled Test Conditions
Testing areas are kept in a controlled environment so results are not affected by temperature swings between day and night.
Scope & Boundaries
What This System Does Not Cover
The rework control system applies to completed or in-process bench vises identified with dimensional, hardness, force, coating or structural defects before shipment release. It does not authorize changes to approved construction, materials, surface finish, product configuration or customer requirements, and it does not cover:
- Products already shipped or in customer channels.
- Structural damage or body deformation not assessed by Engineering.
- Widespread casting defects, forging flaws, or defects that may affect safety.
- Projects where rework is not permitted: customer-approved samples, certification or test units.
- Projects with proprietary customer processes, special materials or special repair requirements.
- Recurring defects that cannot be located, or vises failing again after rework.
Any deviation from customer specifications requires documented engineering review and, where applicable, written customer approval. Vises that cannot be restored to their original specification are only released under an explicit customer concession — never by production alone.
| Method Card | Defect Class | Application Scope | Key Engineering Controls | Sign-off Authority |
|---|---|---|---|---|
| MC-RW-01 | Class A (Surface Finish) | Surface grinding and polishing restoration | Calibrated grinding wheel, controlled feed rate, surface roughness gauge | QC Inspector |
| MC-RW-02 | Class B (Dimensional) | CNC re-machining of jaw seats and bore holes | Coordinate measurement, controlled fixture, approved cutting parameters | QC + Engineering |
| MC-RW-03 | Class C (Hardness) | Re-heat treatment of jaw inserts | Controlled furnace temperature, quench medium, post-quench temper cycle | QC + Engineering |
| MC-RW-04 | Class D (Clamping Force) | Thread re-cutting and jaw alignment correction | Torque-controlled fastening, dial indicator alignment check | Engineering + QA Head |
| MC-RW-05 | Class E (Swivel Mechanism) | Base re-machining and detent repair | Precision jig, controlled torque setting, engagement force test | QC + Engineering |
| MC-RW-06 | Class F (Coating) | Surface re-coating (paint, powder coat, Parkerizing) | Surface preparation, controlled application thickness, cure cycle | Chief Engineer |
| MC-RW-00 | Class G (Critical / Structural) | Mandatory scrap and physical destruction | Physical cut-off to prevent mix-out, scrap record, cross-department root-cause review | Plant Manager |
Third-Party Inspection
Inspector-Friendly Protocol
We provide a dedicated inspection area with calibrated force gauges, hardness testers, precision measuring instruments, and pre-filled Inspection Briefs so third-party agencies (SGS, TÜV, BV, Intertek) can complete pre-shipment inspection efficiently — saving your inspection overhead.
Each brief summarizes the applicable document revisions, approved sample reference, critical-to-quality checks, agreed sampling level, functional tests, and packaging and barcode requirements for the PO. Specified quantities, quality, packing, and basic safety items are verified against the approved project references — no last-minute document hunting on site.
Quality Documentation Pack
Download Sample Quality Pack & Protocol Templates
Standard controlled templates used for OEM/ODM projects — structured as the 00–15 documentation register (project index, approved spec, BOM, artwork & packing references, QIP, inspection records, NCR, change control, third-party brief, release summary).
Quality Documentation Pack (PDF)
Full 00–15 controlled document structure: project index, specification, BOM, artwork and packing references, Quality Inspection Plan (QIP), inspection records, NCR, change control, third-party briefing, and pre-shipment release summary.
Download PDFThird-Party Inspection Brief (PDF)
One-page brief for SGS / TÜV / BV / Intertek inspectors: order quantity, AQL sampling level, applicable revisions, and critical-to-quality checks including clamping force record verification, hardness testing, kit completeness, barcode scan, and carton drop test.
Download PDFChange Control Protocol (PDF)
Change Control Log covering artwork, customer-approved BOM, and carton-marking revisions — with change summary, reason, impact assessment, customer approval status, effective batch, and obsolete document withdrawal.
Download PDFPre-Shipment Release Summary (PDF)
One-page release sign-off: quality gate verification (IQC, IPQC, machining, heat treatment, final inspection, packing), open NCR status, and the authorized release decision signed by quality and operations.
Download PDFRework Change Control Standard (Page)
Formal ISO 9001 change control for rework parameters: ECR, risk classification, cross-department approval matrix, 9-step closed-loop, quantified engineering validation and Poka-Yoke safeguards — with bilingual SOP QMS-SOP-QC-CC-001 Rev 2.0.
View pageNon-Conforming Product Control (Page)
ISO 9001:2015 Clause 8.7 control of non-conforming outputs: NCR registration, quarantine, severity-based disposition authority, controlled rework under SRI, independent re-inspection and witnessed destruction vaulted under SHA-256 — with bilingual SOP and scrap certificate downloads.
View pageFAQ
Frequently Asked Questions About Bench Vise Quality Control
How does Stavalk control bench vise quality?+
Quality is controlled through incoming material inspection, casting and forging inspection, CNC machining verification, heat treatment control, assembly quality checks, final product testing, packing inspection, and production traceability — each executed against project-approved samples, specifications, and inspection criteria.
What quality inspections are performed during bench vise production?+
Inspections include material verification, casting inspection, forging inspection, machining checks, heat treatment hardness testing, assembly verification, clamping force testing, jaw hardness testing, swivel torque verification, appearance inspection, and packing verification.
Can OEM customers request bench vise inspection records?+
Yes. Inspection records and quality documentation can be provided according to project requirements and customer quality agreements, including sample pre-shipment inspection reports.
How does the factory ensure OEM production consistency?+
Production consistency is maintained through approved samples, technical specifications, manufacturing checkpoints, inspection procedures, and documented quality control processes linked to each order.
Can I arrange third-party inspection by SGS, TÜV, BV, or Intertek?+
Yes. We host third-party inspectors with a dedicated inspection area, calibrated force gauges, hardness testers, pre-filled inspection briefs, and accessible records. Share your specification, approved sample, artwork, packaging requirements, and defect criteria — or use our Third-Party Inspection Brief template.
How are artwork, BOM, or packaging changes handled during production?+
Changes are logged in our Change Control Log with the affected document revision, change summary, reason, impact assessment, customer approval status, and effective batch. Obsolete versions are withdrawn so production and inspection always use the current approved documents.
Does the factory support customized bench vise projects?+
Yes. Customized bench vise OEM/ODM projects are supported based on customer specifications, artwork requirements, accessory configurations, and packaging needs, with project-specific inspection criteria agreed before production.
Can a defective bench vise be reworked at the factory?+
Yes — under controlled conditions. The vise is placed on HOLD and linked to an NCR, the defect is located with an approved diagnostic method, and rework proceeds only after QC/Engineering authorization and only within the defect classes approved for rework. The vise is then re-inspected against the same acceptance criteria as a conforming product before release.
How many times can the factory rework a vise?+
A single location may be reworked once under an authorized instruction. If re-inspection still fails, the vise is escalated for replacement, rejection, scrap, or customer concession — repeated rework without documented approval is not permitted.
Need a Complete Project Quality Pack Sample?
Request an anonymized Third-Party Inspection Support Pack and Quality Inspection Plan (QIP) for your OEM/ODM project — or download the sample templates to review the documentation structure you can expect for your order.